Precision Gear Shaper Cutters
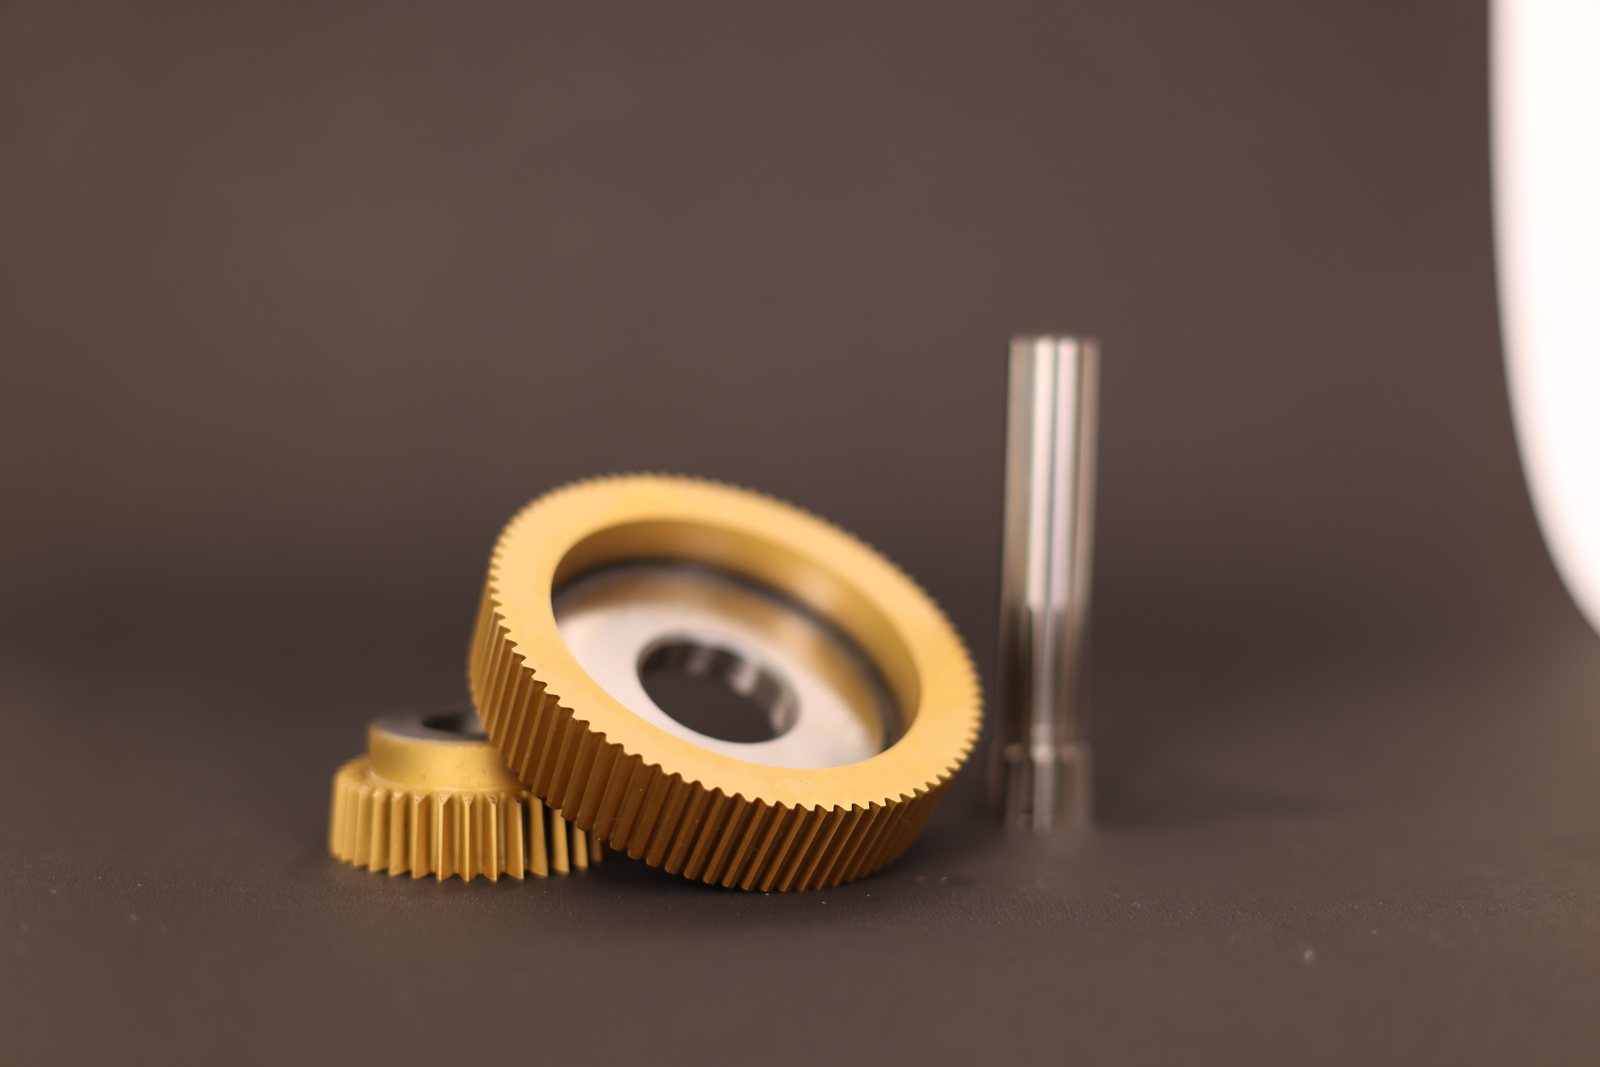
CTI shaper cutters generate internal and external spur and helical gears, splines, sprockets and timing pulleys from module 0.5 to 20 (50 DP to 1.25 DP), up to 300 mm (12") diameter, in DIN 1829 accuracy class AA, A or B. They are supplied as disc, hub (deep-counterbore), shank or bell types in M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy) with TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Custom cutters for pre-shaving and pre-grinding (protuberance and semi-topping) are routine.
Types of gear shaper cutters
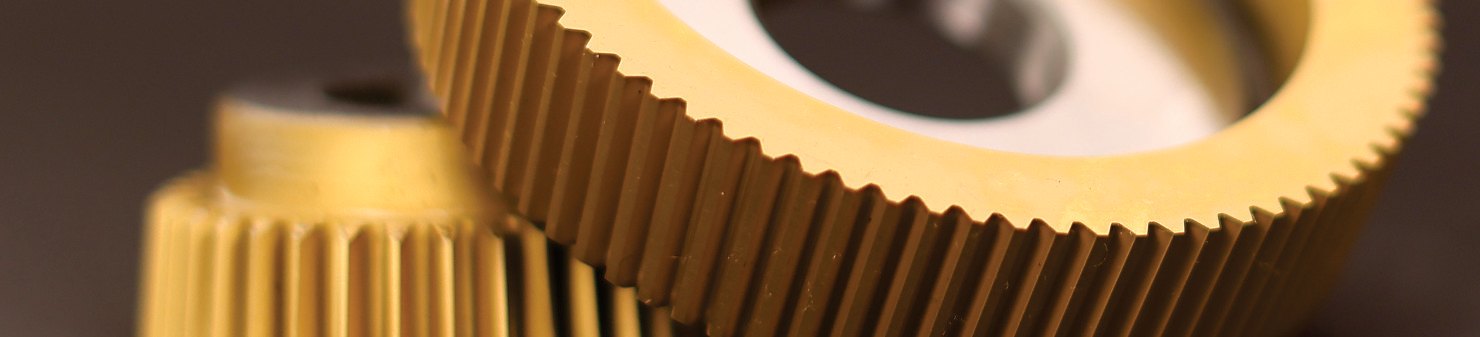
- Disc-type cutters: the workhorse for external spur and helical gears; bore-mounted, with the most usable face for resharpening and the lowest cost per piece over the cutter's life.
- Deep counterbore (hub-type) cutters: an extended hub gives clearance when the gear sits close to a shoulder, flange or another gear in a cluster.
- Shank-type cutters: an integral taper or straight shank for internal gears with small pitch diameters, where a bore-mounted cutter will not fit.
- Bell-type cutters: a deeper hub for parts with extra-long shoulder-clearance demands.
Not sure which type clears your part? Our engineers draw the cutter into the part envelope and confirm clearance at the deepest stroke position before we quote.
When shaping is the right process
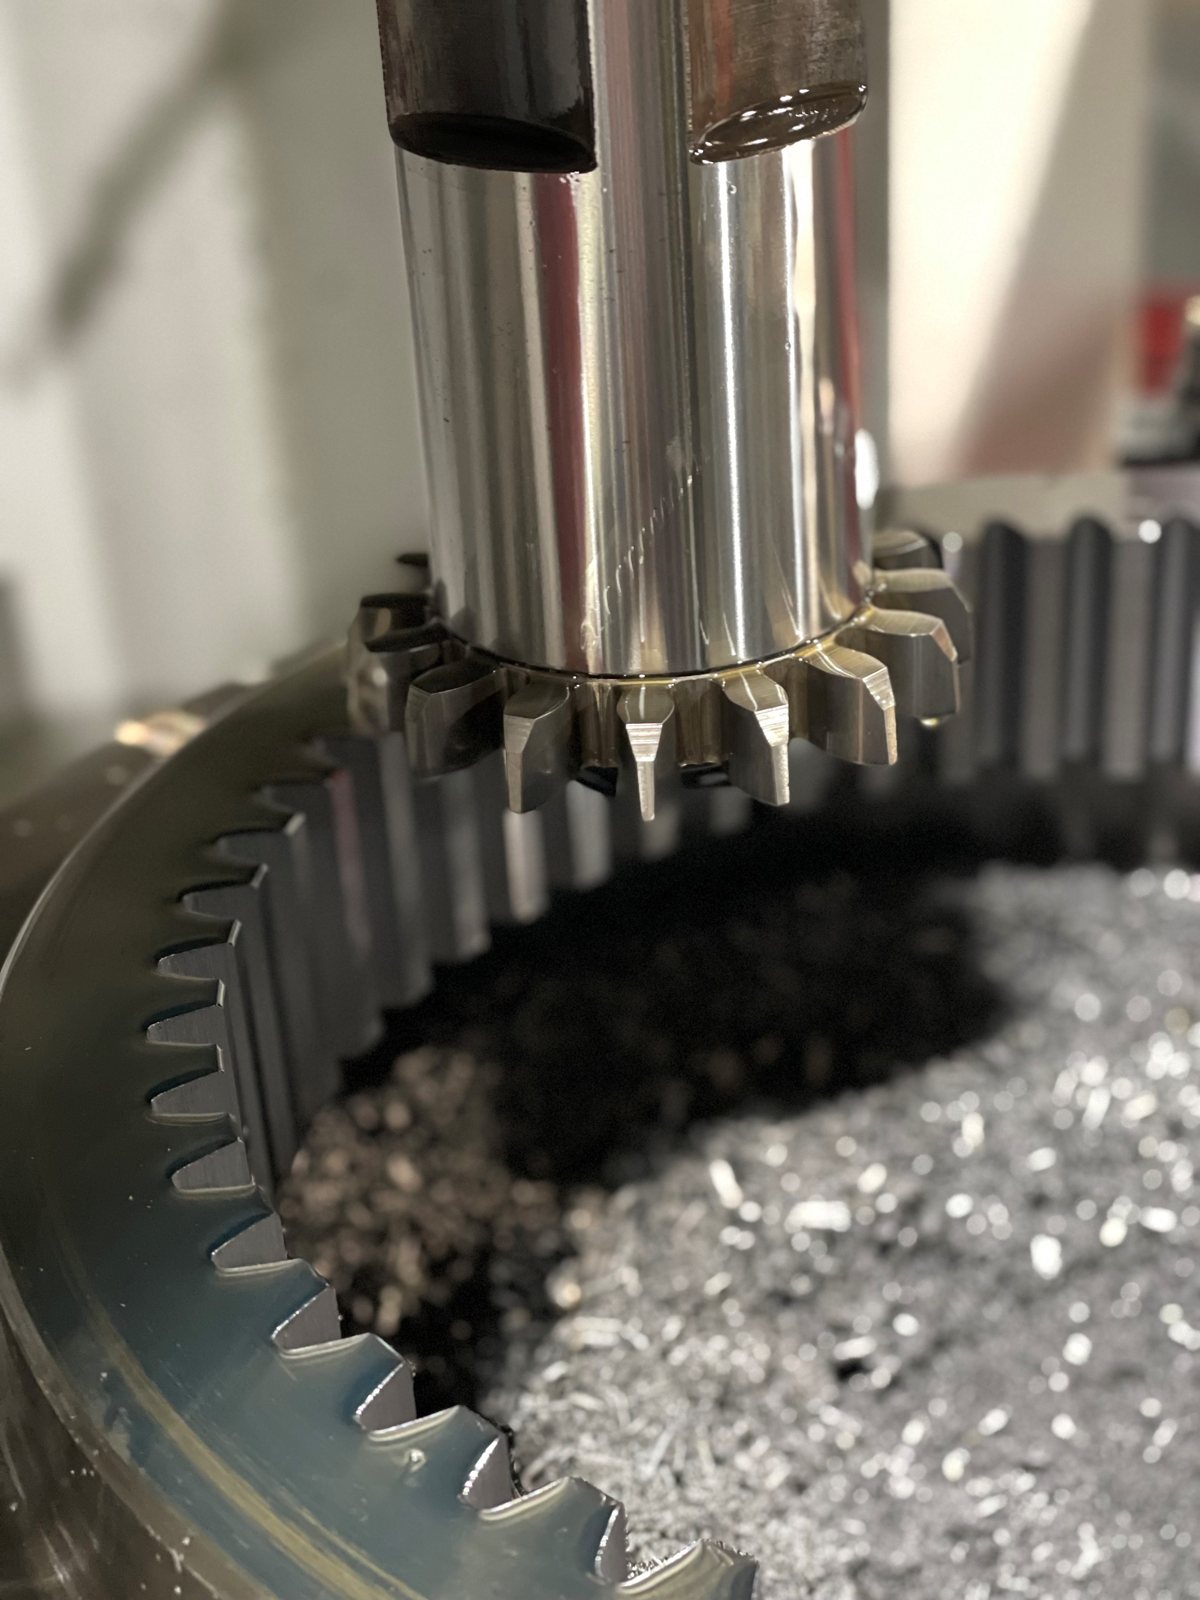
Hobbing is usually faster for external gears with open access on both sides. Shaping wins when the geometry blocks a hob: internal ring gears, cluster gears, shoulder gears with little overrun, sector gears and stepped profiles. If the part can be hobbed without compromise, hob it; if it cannot, shaping is the path. Read our guide, Selecting the Right Gear Shaper Cutter, for the full decision process.
Why buy CTI tooling through CTI-USA
- Clearance checked before we quote. We draw the cutter into your part envelope and confirm shoulder, hub and stroke clearance, so the cutter that arrives fits the part and the machine.
- One manufacturer, every gear cutting tool. Hobs, shaper cutters, power skiving cutters, broaches and milling cutters from Capital Tool Industries, a single ISO 9001 source in Patiala, India, so profiles and tolerances are consistent across your process.
- Materials and coatings that fit the job. M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy); TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Our engineers recommend the combination for your workpiece, hardness and volume. Properly specified coatings typically extend tool life 3–8× compared with uncoated tools.
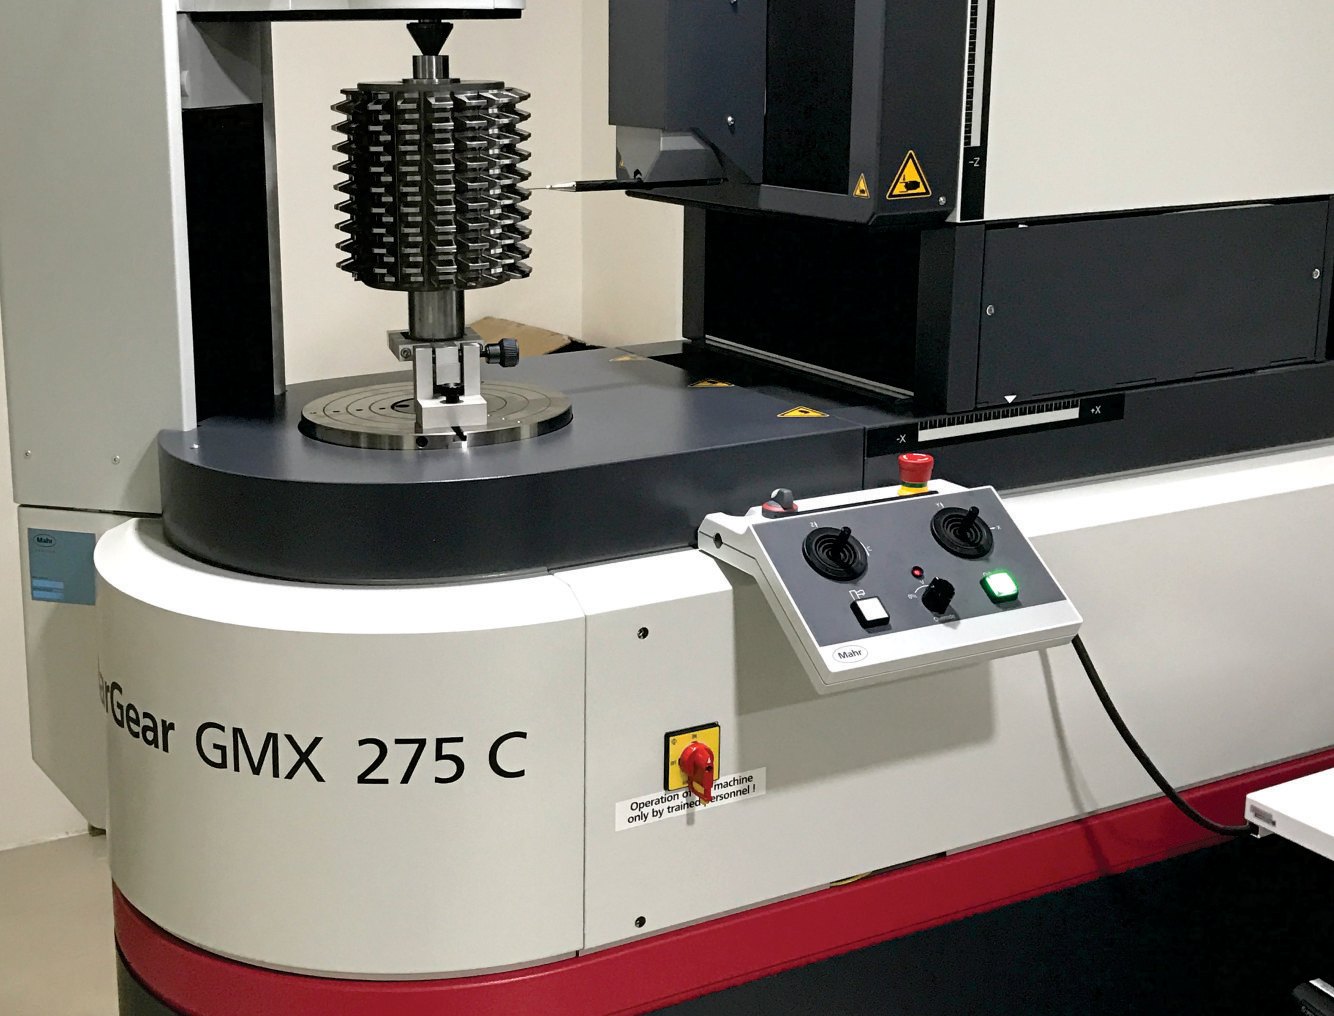
- Inspection you can read. Each tool is measured on Klingelnberg equipment and ships with its report.
- US-based support. Prints, technical questions and quotes are handled from Hudson, Ohio (Monday–Friday, 8:00 am–5:00 pm Eastern); we reply within one business day. Typical lead time is 6–8 weeks.
- Resharpening and recoating. We arrange resharpening and recoating of hobs, shaper cutters and broaches of any make, so you get the full regrind life out of every one.
Applications
- Automotive: transmission, differential and drive-system gears, especially internal ring gears and cluster gears.
- Aerospace: lightweight, high-accuracy gear components.
- Heavy machinery: robust gears for industrial equipment.
Shaper cutters vs. gear hobs
- Shaper cutters reciprocate against the blank while both rotate in time, so they can cut internal gears and gears next to a shoulder.
- Gear hobs cut with a continuous rotary motion and are faster for external gears in volume.
CTI-USA supplies both, so the recommendation is driven by your part, not by what we have to sell.
Sharpening
A shaper cutter is sharpened on its rake face, and each regrind shortens the cutter. CTI-USA offers resharpening and recoating that preserves rake and relief angles so the cutter continues to cut to its rated class, and we can advise on the minimum usable length for each cutter we supply.
Estimate your cycle time
Use the free shaping cycle-time estimator for external gears or internal splines on CNC gear shapers, then request a quote from the result.
Send us a print
Email a part drawing or tool drawing to sales@cti-usa.co or use the request-a-quote form (PDF, DWG, DXF, STEP, IGES or an image, up to 8 MB through the request form; larger files by email (ask for a transfer link over 20 MB)). Tell us the gear or spline data, the part drawing showing shoulders and clusters, your shaper spindle and stroke, material and hardness, and annual volume, and we will recommend a tool steel and coating with the quote. We reply within one business day; typical lead time is 6–8 weeks.
Frequently asked questions
What is the difference between disc, hub and shank shaper cutters?
Disc cutters are flat and bore-mounted for general external work. Hub (deep counterbore) cutters add an extended hub for shoulder clearance. Shank cutters have an integral taper or straight shank for small internal gears where a bore-mounted cutter cannot fit.
What size shaper cutters does CTI make?
Module 0.5 to 20 (50 DP to 1.25 DP), up to 300 mm (12 inches) in diameter.
What accuracy class do I need?
DIN 1829 class AA for ground gears and master gears, class A for most precision production such as automotive transmissions, and class B for general industrial gearing that is heat-treated and finished after shaping.
Can a shaper cutter cut helical gears?
Yes. The cutter is ground to the gear's helix angle, of opposite hand for external gears and the same hand for internal gears, and the shaping machine uses a helical guide to impart the lead during the stroke.
Do you make pre-shave and pre-grind cutters?
Yes. Protuberance and semi-topping cutters for pre-shaving and pre-grinding are standard options.
How many times can a shaper cutter be resharpened?
It depends on the cutter type and the material removed per grind. Disc cutters offer the most regrinds. CTI-USA's resharpening service removes the minimum material needed and tells you the remaining usable length.
Related pages and guides
Send us a print and we will get started.
Our engineers will recommend the tool steel and coating for your job and quote it. Typical lead time 6–8 weeks.