Precision Gear Hobs for Spur and Helical Gears
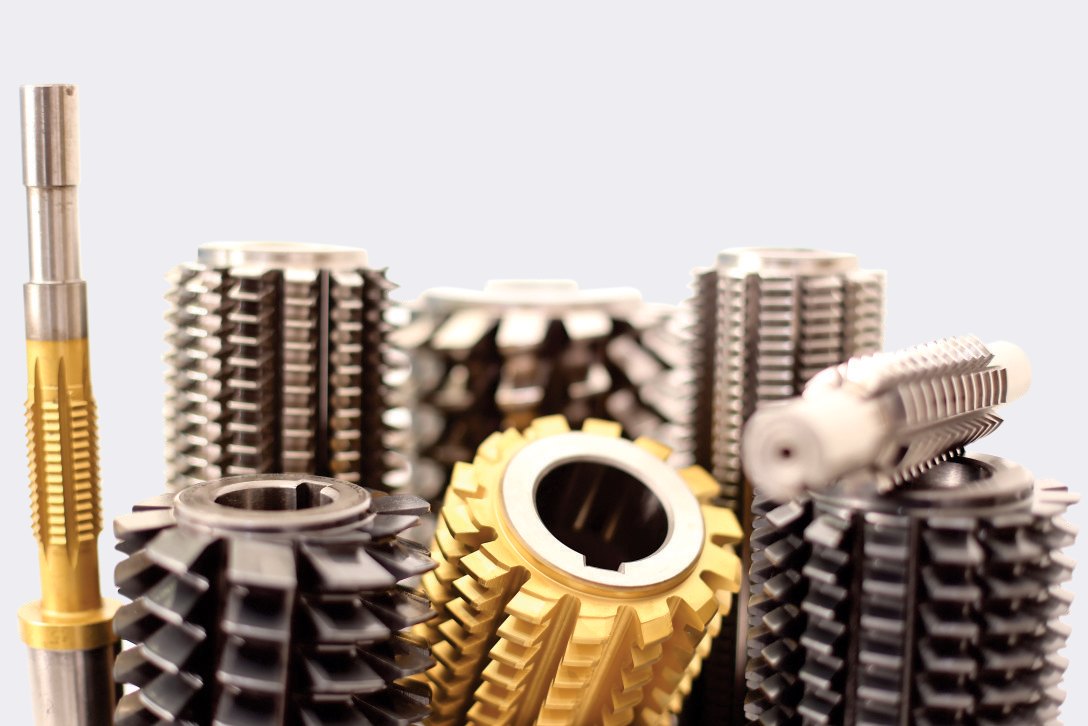
CTI gear hobs cut spur and helical gears from module 0.1 to 40 (inch pitches from 120 DP to 0.7 DP), in DIN 3968 accuracy class AA, A or B, with any profile modification your print calls for: protuberance, chamfering, topping or tip relief. Hobs are made in M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy) with TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings, and are supplied by CTI-USA from Hudson, Ohio with a typical lead time of 6–8 weeks.
Types of gear hobs
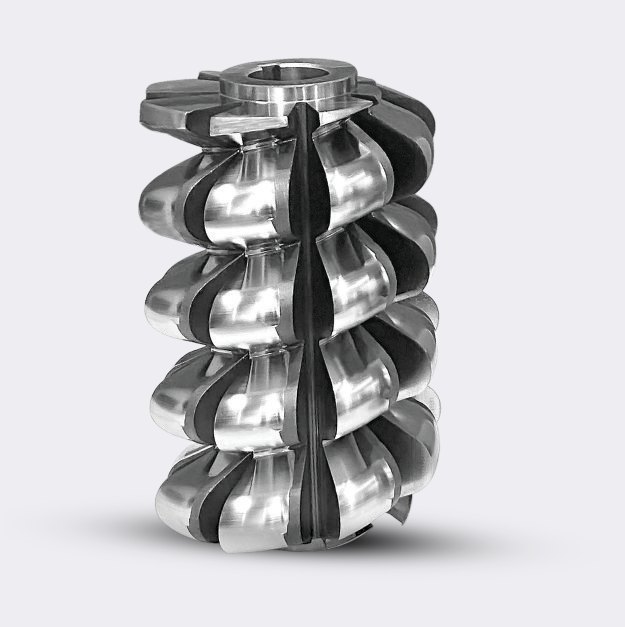
Single-start gear hobs
- The standard choice for accurate tooth form and minimal profile variation.
- Right for small-batch and standard gear production.
Multi-start gear hobs
- Two or more threads for higher table feed and shorter cycle times.
- Best for high-volume work where the gear will be finished afterwards or where class B accuracy is acceptable.
Custom gear hobs
- Built to your print, including protuberance, chamfering, topping and tip relief.
- Single or multi-start, DIN 3968 class AA, A or B.
Straight and involute spline hobs
- For parallel or involute splines, straight or helical.
- Semi-topping, undercutting and shoulder clearance available.
- Standards: DIN 5480, 5481, 5482; NF E 22-141; ANSI B92.1; power take-off shafts to DIN 9611.
Chain sprocket and timing pulley hobs
- Roller-chain sprocket hobs to ANSI, BS, IS or custom standards, ground or unground profile. See chain sprocket hobs.
- Timing pulley hobs for classical trapezoidal (ISO 5294), metric T/AT (DIN 7721), HTD, PowerGrip GT and Synchroflex belts. See timing pulley hobs.
Worm gear hobs
- Flank forms ZN, ZA, ZI, ZK and ZC up to 45° lead angle; hollow (bore) or integral-shank; tangential, radial, topping or non-topping. See worm gear hobs.
Why buy CTI tooling through CTI-USA
- Regrind life designed in. Relief angles and gash counts are chosen for your production and resharpening program, not a catalog default, so each hob gives the most regrinds between retirements.
- One manufacturer, every gear cutting tool. Hobs, shaper cutters, power skiving cutters, broaches and milling cutters from Capital Tool Industries, a single ISO 9001 source in Patiala, India, so profiles and tolerances are consistent across your process.
- Materials and coatings that fit the job. M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy); TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Our engineers recommend the combination for your workpiece, hardness and volume. Properly specified coatings typically extend tool life 3–8× compared with uncoated tools.
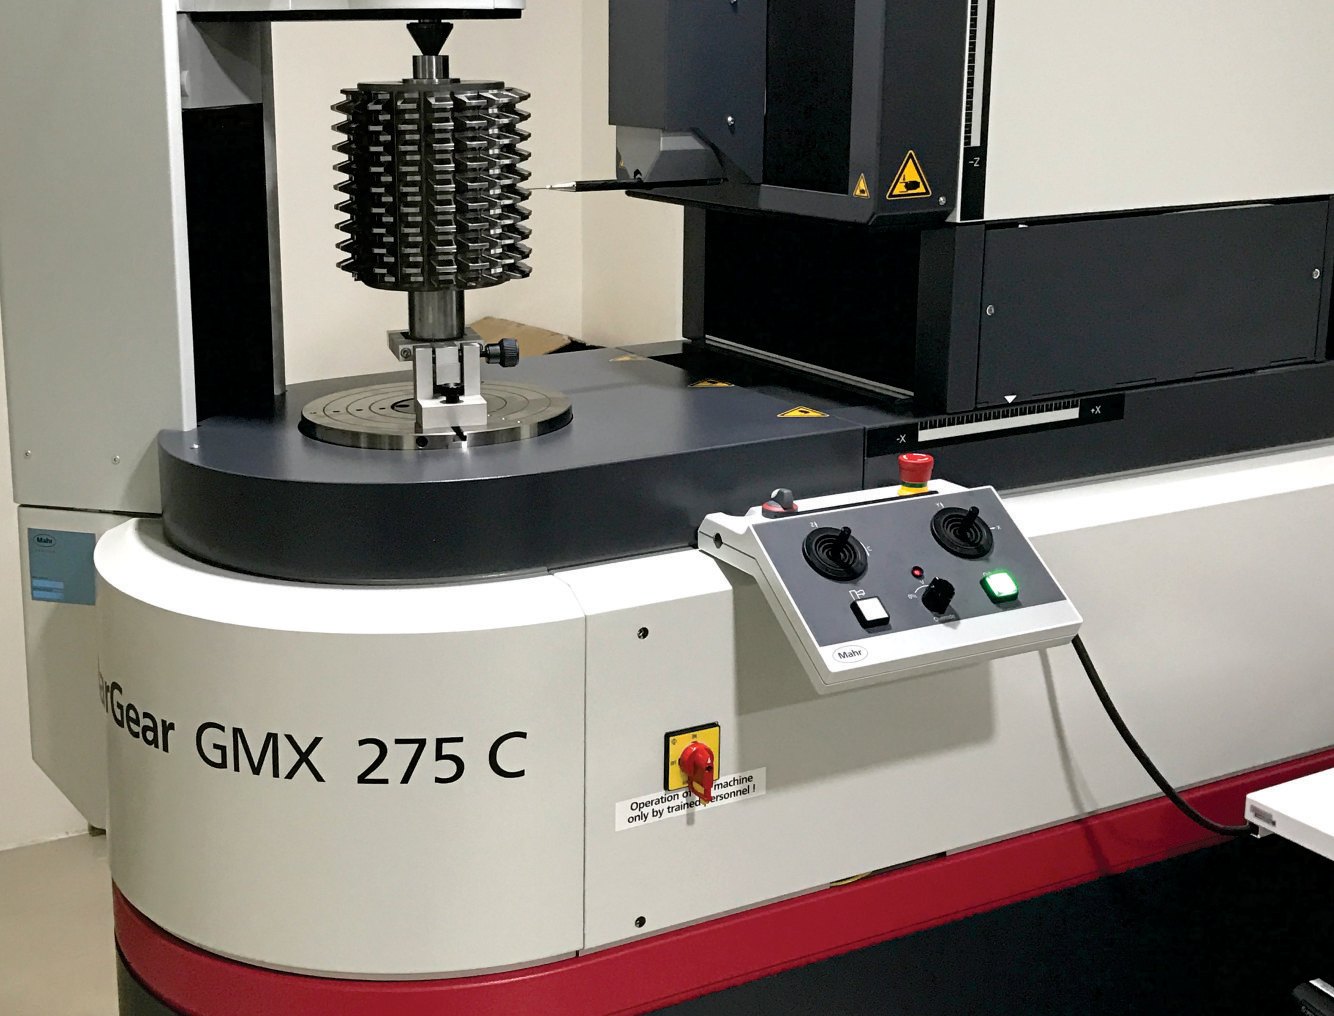
- Inspection you can read. Each tool is measured on Klingelnberg equipment and ships with its report.
- US-based support. Prints, technical questions and quotes are handled from Hudson, Ohio (Monday–Friday, 8:00 am–5:00 pm Eastern); we reply within one business day. Typical lead time is 6–8 weeks.
- Resharpening and recoating. We arrange resharpening and recoating of hobs, shaper cutters and broaches of any make, so you get the full regrind life out of every one.
Applications
- Automotive: transmission and driveline gears.
- Aerospace: precision gear components for aircraft systems.
- Heavy machinery: industrial and construction equipment gearing.
- Power transmission: gearboxes, pumps and energy systems.
How CTI makes a gear hob
- Material selection: M2, M35 or a powder-metallurgy grade (ASP 2030/2052/2060, S290, S390) chosen for your workpiece hardness and volume.
- Profile design: engineered from your gear print, including any protuberance, chamfer or tip relief.
- CNC machining and relief grinding: in-house heat treatment, CNC relief grinding and finish grinding.
- Coating: PVD coating matched to the application.
- Inspection: measured on Klingelnberg gear measuring centers; report ships with the tool.
Not sure which hob you need?
Run the free hobbing cycle-time estimator to compare single- and multi-start options for your part, or use the tool steel and coating selector to see which grade and coating fit your material. Both end with a one-click quote request.
Send us a print
Email a part drawing or tool drawing to sales@cti-usa.co or use the request-a-quote form (PDF, DWG, DXF, STEP, IGES or an image, up to 8 MB through the request form; larger files by email (ask for a transfer link over 20 MB)). Tell us the gear data (module or DP, pressure angle, teeth, helix, face width), the workpiece material and hardness, annual volume, and wet or dry cutting, and we will recommend a tool steel and coating with the quote. We reply within one business day; typical lead time is 6–8 weeks.
Frequently asked questions
What accuracy classes are CTI gear hobs made to?
DIN 3968 class AA, A or B. Class AA is for ground or master-quality gears, class A for most precision production, and class B for general industrial gearing that will be finished after hobbing.
What size range do you cover?
Module 0.1 to 40 in metric pitches and 120 DP to 0.7 DP in inch pitches, with hob diameters from roughly 0.75 to 15 inches. Larger or smaller sizes are quoted on request.
Which tool steel should I choose?
M2 is the general-purpose grade for mild and low-alloy steels. M35 (cobalt) holds its edge longer in alloy steels. The powder-metallurgy grades ASP 2030, 2052 and 2060, S290 and S390 give the longest life on hardened or abrasive work and in high-volume dry hobbing. M42 and solid carbide are quoted on request. Send us the workpiece material and hardness and we will recommend a grade.
Which coating should I choose?
TiN for general wet hobbing of carbon steels, TiCN for abrasive materials and cast iron, TiAlN for alloy steels and dry cutting, AlCrN (Alcrona) for the highest temperatures and oxidation resistance, and Altensa for high-productivity hobbing of case-hardening steels. Properly matched coatings typically extend tool life 3–8×.
What is the lead time on a gear hob?
Typically 6–8 weeks for a custom hob. Lead time is confirmed on every quote.
Do you stock hobs, and can you expedite?
Every tool is made to order; we do not carry stock. If you need a hob in under six weeks, call 330-962-8160 before sending the print and we will tell you whether it can be done and what expediting costs.
How do I order?
Send the print; we quote within one business day. On your purchase order (made out to Potesta Consulting Group LLC dba CTI-USA) CTI prepares a tool drawing for your approval, then manufactures, inspects and ships. Payment terms are stated on every quote; open account is available on approved credit (credit application on request). W-9 and the Capital Tool Industries ISO 9001 certificate are available on request.
Where are the hobs made?
Patiala, India, by Capital Tool Industries (ISO 9001); engineering, quoting and support from Hudson, Ohio.
Can you resharpen and recoat my hobs?
Yes. CTI-USA provides resharpening to original geometry and recoating for hobs, shaper cutters and broaches. See the sharpening and recoating page.
Related pages and guides
Send us a print and we will get started.
Our engineers will recommend the tool steel and coating for your job and quote it. Typical lead time 6–8 weeks.