Spline Hobs and Spline Cutting Tools
CTI spline hobs cut external involute and parallel splines and serrations, straight or helical, to DIN 5480 and 5482, DIN 5481 (serrations), NF E 22-141, ANSI B92.1 and DIN 9611 power take-off shafts, with semi-topping, undercutting and shoulder clearance as required. Internal splines are cut with CTI shaper cutters or broaches. All tools are made in M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy) with TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings.
External spline tools: hobs
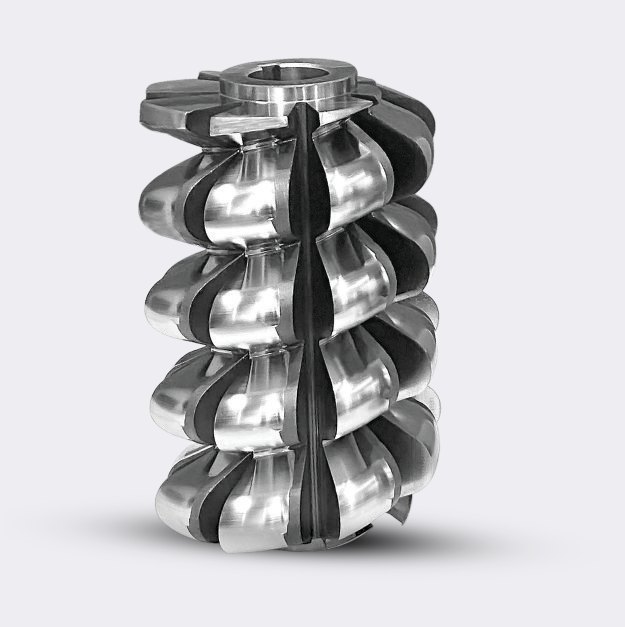
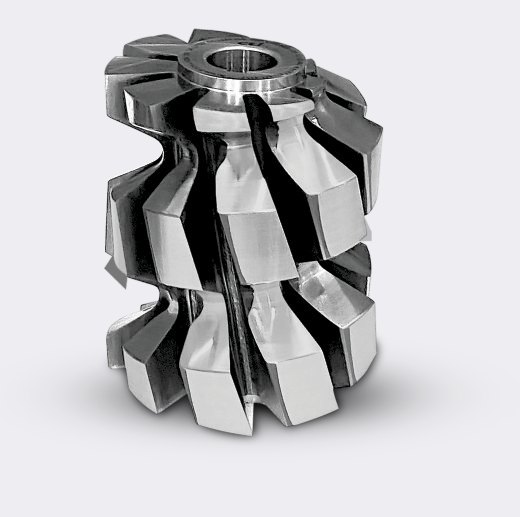
- Involute spline hobs to DIN 5480 and 5482, NF E 22-141 and ANSI B92.1; serration hobs to DIN 5481.
- Parallel (straight-sided) spline hobs with or without lugs, semi-topping and shoulder clearance.
- Power take-off shaft hobs to DIN 9611.
- Available in single or multi-start, DIN 3968 class AA, A or B.
Internal spline tools: shaper cutters and broaches
Internal splines cannot be hobbed. CTI-USA supplies:
- Spline shaper cutters (disc, hub or shank type) for internal splines in gear shaping machines. Shank-type cutters reach small internal diameters. See gear shaper cutters.
- Spline broaches for high-volume internal splines in a single pass. See broaches.
Applications
- Automotive: transmission, drivetrain and axle splines.
- Agriculture and off-highway: PTO shafts and drive splines.
- Aerospace: high-performance coupling splines.
- Industrial machinery: interlocking shafts and couplings.
Why buy CTI tooling through CTI-USA
- Internal and external from one source. Spline hobs for the shaft and shaper cutters or broaches for the mating bore, specified together so the fit is right.
- One manufacturer, every gear cutting tool. Hobs, shaper cutters, power skiving cutters, broaches and milling cutters from Capital Tool Industries, a single ISO 9001 source in Patiala, India, so profiles and tolerances are consistent across your process.
- Materials and coatings that fit the job. M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy); TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Our engineers recommend the combination for your workpiece, hardness and volume. Properly specified coatings typically extend tool life 3–8× compared with uncoated tools.
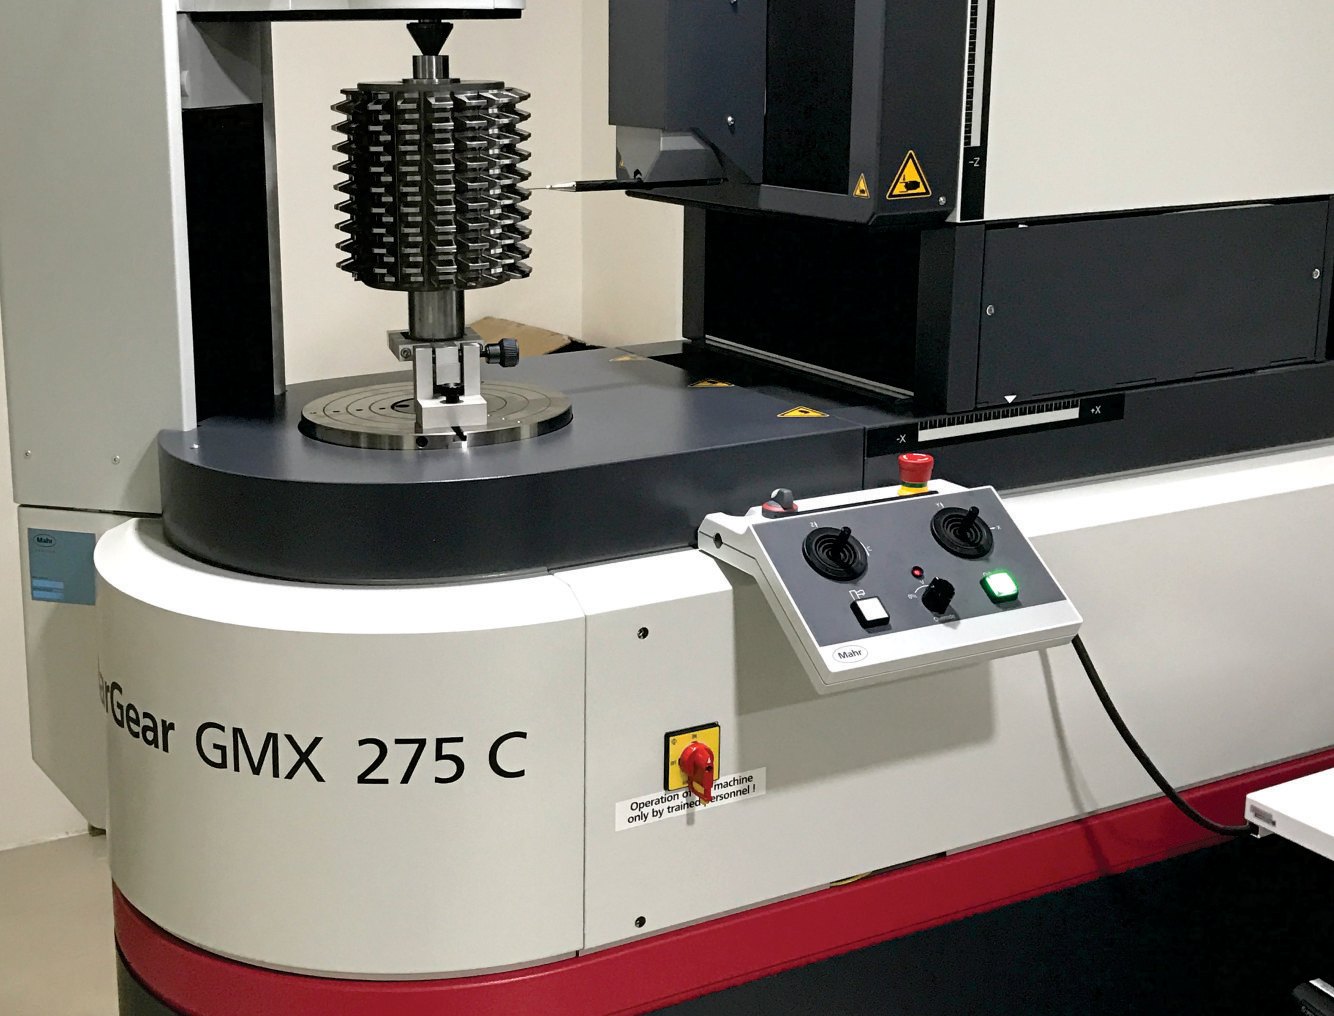
- Inspection you can read. Each tool is measured on Klingelnberg equipment and ships with its report.
- US-based support. Prints, technical questions and quotes are handled from Hudson, Ohio (Monday–Friday, 8:00 am–5:00 pm Eastern); we reply within one business day. Typical lead time is 6–8 weeks.
- Resharpening and recoating. We arrange resharpening and recoating of hobs, shaper cutters and broaches of any make, so you get the full regrind life out of every one.
Estimate your spline cycle time
Shaping an internal spline? Use the free shaping cycle-time estimator, which handles internal splines on CNC gear shapers. Hobbing an external spline? Use the hobbing estimator. Both end with a one-click quote request.
Send us a print
Email a part drawing or tool drawing to sales@cti-usa.co or use the request-a-quote form (PDF, DWG, DXF, STEP, IGES or an image, up to 8 MB through the request form; larger files by email (ask for a transfer link over 20 MB)). Tell us the spline standard and designation, number of teeth, straight or helical, internal or external, material and hardness, and annual volume, and we will recommend a tool steel and coating with the quote. We reply within one business day; typical lead time is 6–8 weeks.
Frequently asked questions
Can an internal spline be hobbed?
No. Hobs need clearance to run past the work, so internal splines are cut with shaper cutters or broaches. CTI-USA supplies both.
Which spline standards do you cover?
DIN 5480, DIN 5481, DIN 5482, NF E 22-141, ANSI B92.1 and DIN 9611 for power take-off shafts, plus custom forms to your print.
What is semi-topping?
A small chamfer cut at the tip of the spline tooth in the same pass, which removes burrs and avoids a secondary deburring operation.
What tool steel and coating should I use for splines?
For most spline hobbing in carbon and alloy steel, M35 or ASP 2030 with TiAlN or Alcrona is a good starting point; high-volume dry hobbing favors ASP 2052 or S390 with Altensa. Send the material and volume and we will recommend.
Related pages and guides
Send us a print and we will get started.
Our engineers will recommend the tool steel and coating for your job and quote it. Typical lead time 6–8 weeks.