Precision Broaches for Internal Profiles, Made to Your Print
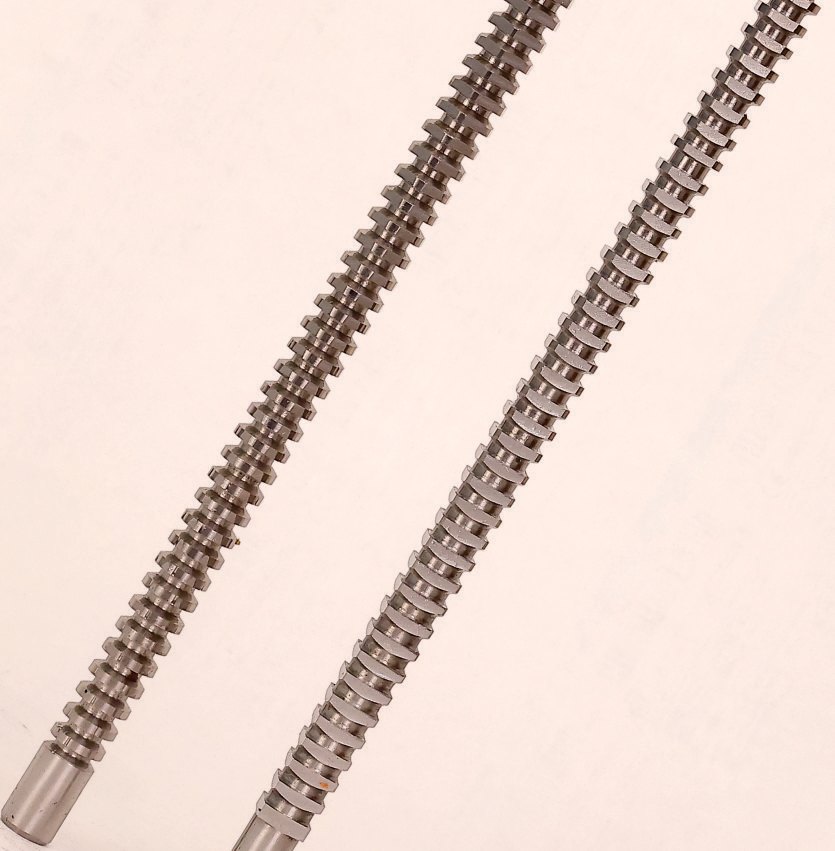
Capital Tool Industries is a broach manufacturer supplying standard and special broaches in push and pull styles for involute, parallel and trapezoidal splines, serrations, round, hexagonal and rectangular holes, keyways and ratchet forms. Every broach is designed to your component specification, machine and holder details, in M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy) with TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings, and supplied by CTI-USA with a typical lead time of 6–8 weeks.
Types of broaches
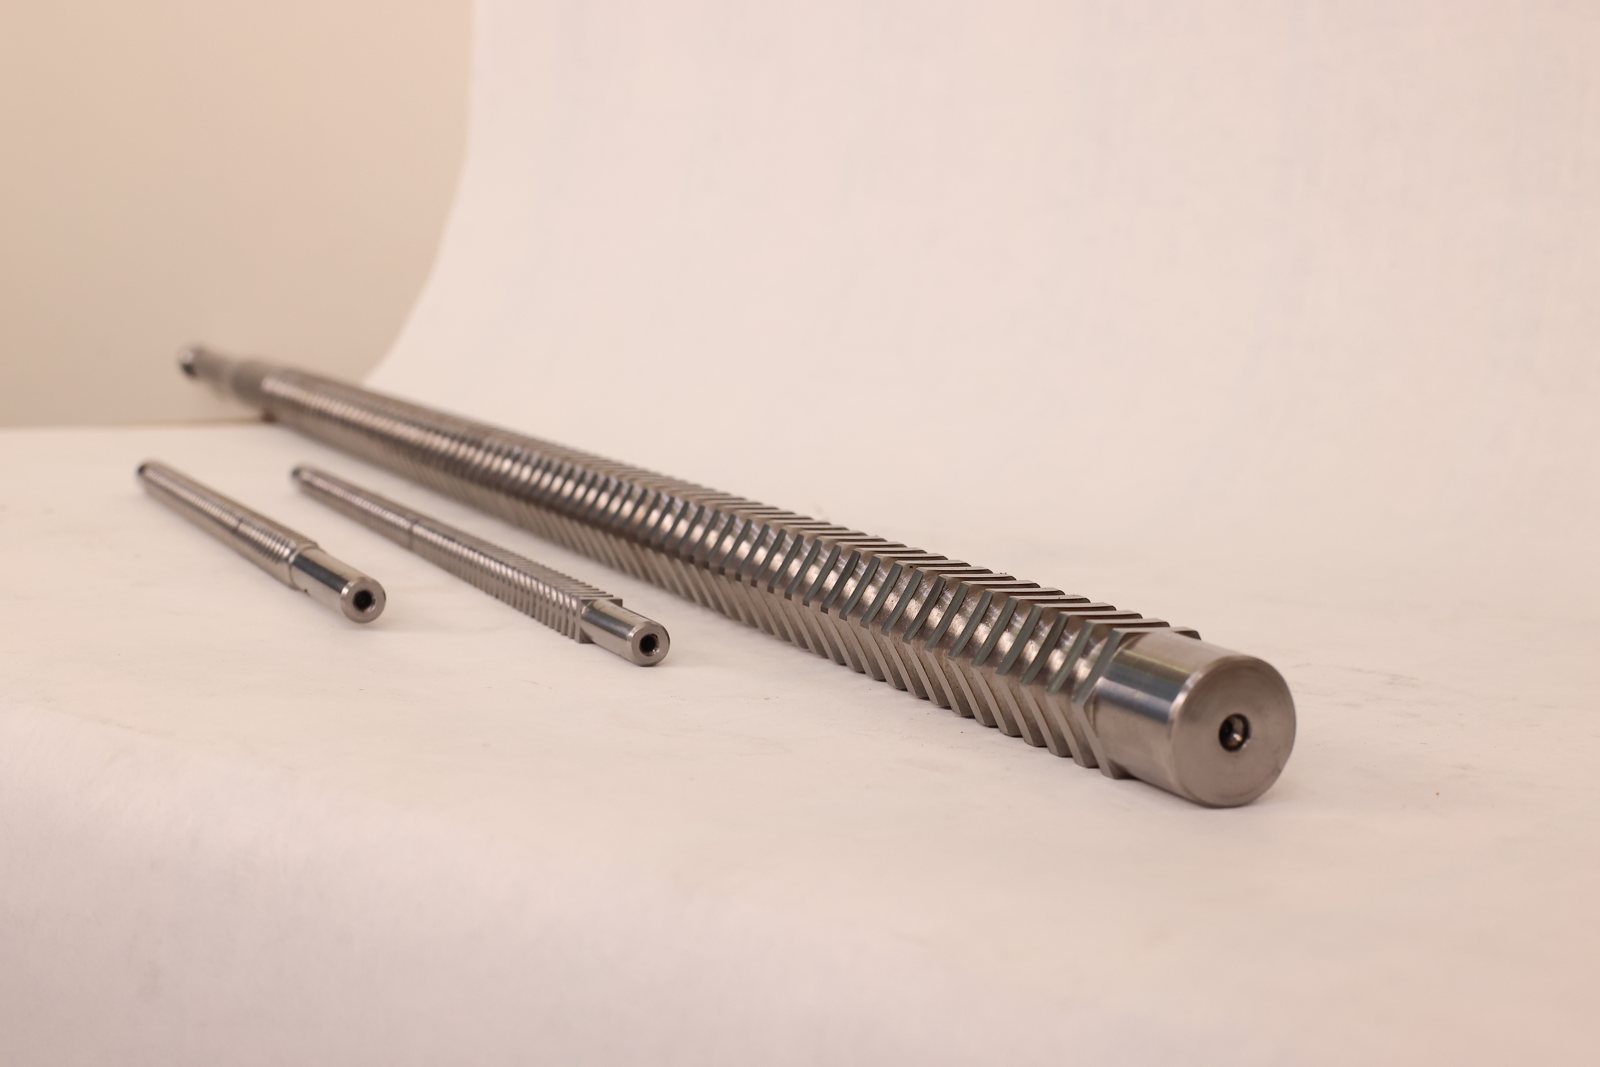
- Push-type broaches: pushed through the part on a press or vertical broaching machine; typically shorter tools for shallower profiles.
- Pull-type broaches: drawn through the part on a horizontal or vertical pull-down machine; the usual choice for longer cuts and production work.
Broach profiles available
- Spline broaches: involute, parallel and trapezoidal splines for transmission and rotational applications.
- Serration broaches: interlocking toothed profiles.
- Round broaches: cylindrical holes with a sized, smooth finish.
- Hexagonal broaches: hex sockets for fasteners and interlocking components.
- Rectangular and keyway broaches: slots and keyways.
- Special form broaches: ratchet forms and other custom internal profiles.
What we need to quote a broach
- The component print (or the feature to be broached: profile, length of cut, tolerance class).
- Workpiece material and hardness at broaching.
- Broaching machine: push or pull, stroke and tonnage.
- Holder or puller details (shank style and dimensions).
- Annual volume, so we can recommend the tool steel and coating.
Why buy CTI tooling through CTI-USA
- Designed to your machine, not just your part. Every broach is laid out around your press or broaching machine stroke and tonnage and your puller or holder details.
- One manufacturer, every gear cutting tool. Hobs, shaper cutters, power skiving cutters, broaches and milling cutters from Capital Tool Industries, a single ISO 9001 source in Patiala, India, so profiles and tolerances are consistent across your process.
- Materials and coatings that fit the job. M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy); TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Our engineers recommend the combination for your workpiece, hardness and volume. Properly specified coatings typically extend tool life 3–8× compared with uncoated tools.
- Inspection you can read. Each tool is measured on Klingelnberg equipment and ships with its report.
- US-based support. Prints, technical questions and quotes are handled from Hudson, Ohio (Monday–Friday, 8:00 am–5:00 pm Eastern); we reply within one business day. Typical lead time is 6–8 weeks.
- Resharpening and recoating. We arrange resharpening and recoating of hobs, shaper cutters and broaches of any make, so you get the full regrind life out of every one.
Resharpening
A broach is sharpened on the face of each tooth, preserving the rise per tooth and the relief. CTI-USA offers resharpening and recoating for broaches of any make, including those we did not supply.
Send us a print
Email a part drawing or tool drawing to sales@cti-usa.co or use the request-a-quote form (PDF, DWG, DXF, STEP, IGES or an image, up to 8 MB through the request form; larger files by email (ask for a transfer link over 20 MB)). Tell us the component print, workpiece material and hardness at broaching, push or pull machine with stroke and tonnage, holder or puller details, and annual volume, and we will recommend a tool steel and coating with the quote. We reply within one business day; typical lead time is 6–8 weeks.
Frequently asked questions
What is a broach?
A broach is a multi-tooth cutting tool in which each tooth is slightly larger than the one before it, so the full profile is cut in a single pass. Broaches produce internal splines, keyways, round and hexagonal holes and other forms that are difficult to machine any other way.
What is the difference between push-type and pull-type broaches?
Push broaches are forced through the workpiece, usually on a press, and are shorter. Pull broaches are drawn through the part on a broaching machine and are used for longer cuts and production volumes.
What materials are CTI broaches made from?
M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy). Coatings include TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings.
Can you make a broach from my component drawing?
Yes. Send the component print, the workpiece material and hardness, the machine type and the holder details, and we will design the broach and quote it.
How often does a broach need resharpening?
It depends on the workpiece material, the length of cut and the finish required. CTI-USA can resharpen and recoat broaches and will advise on the expected pieces per sharpening for your application.
Related pages and guides
Send us a print and we will get started.
Our engineers will recommend the tool steel and coating for your job and quote it. Typical lead time 6–8 weeks.