Worm Gear Hobs
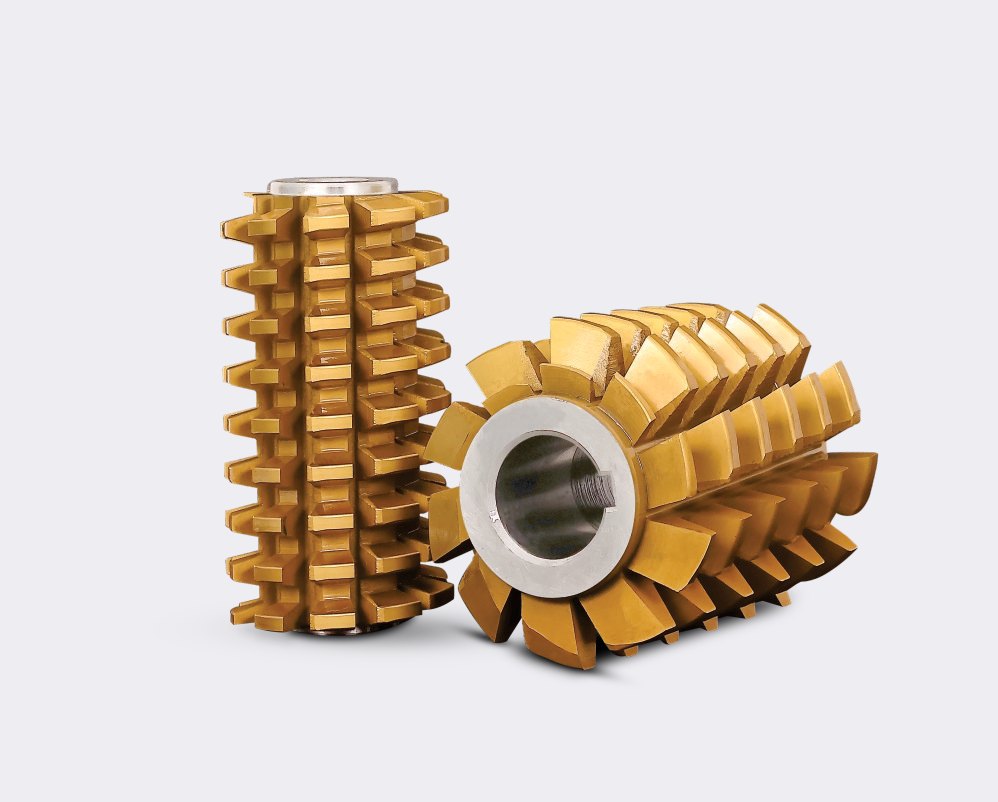
CTI worm gear hobs are supplied for flank forms ZN, ZA, ZI, ZK and ZC up to a 45° lead angle, as hollow (bore-type) or integral-shank hobs, in tangential, radial, topping or non-topping designs, with special reaming-type finishing hobs also available. They are made in M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy) with TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings and supplied by CTI-USA with a typical lead time of 6–8 weeks.
Types of worm gear hobs
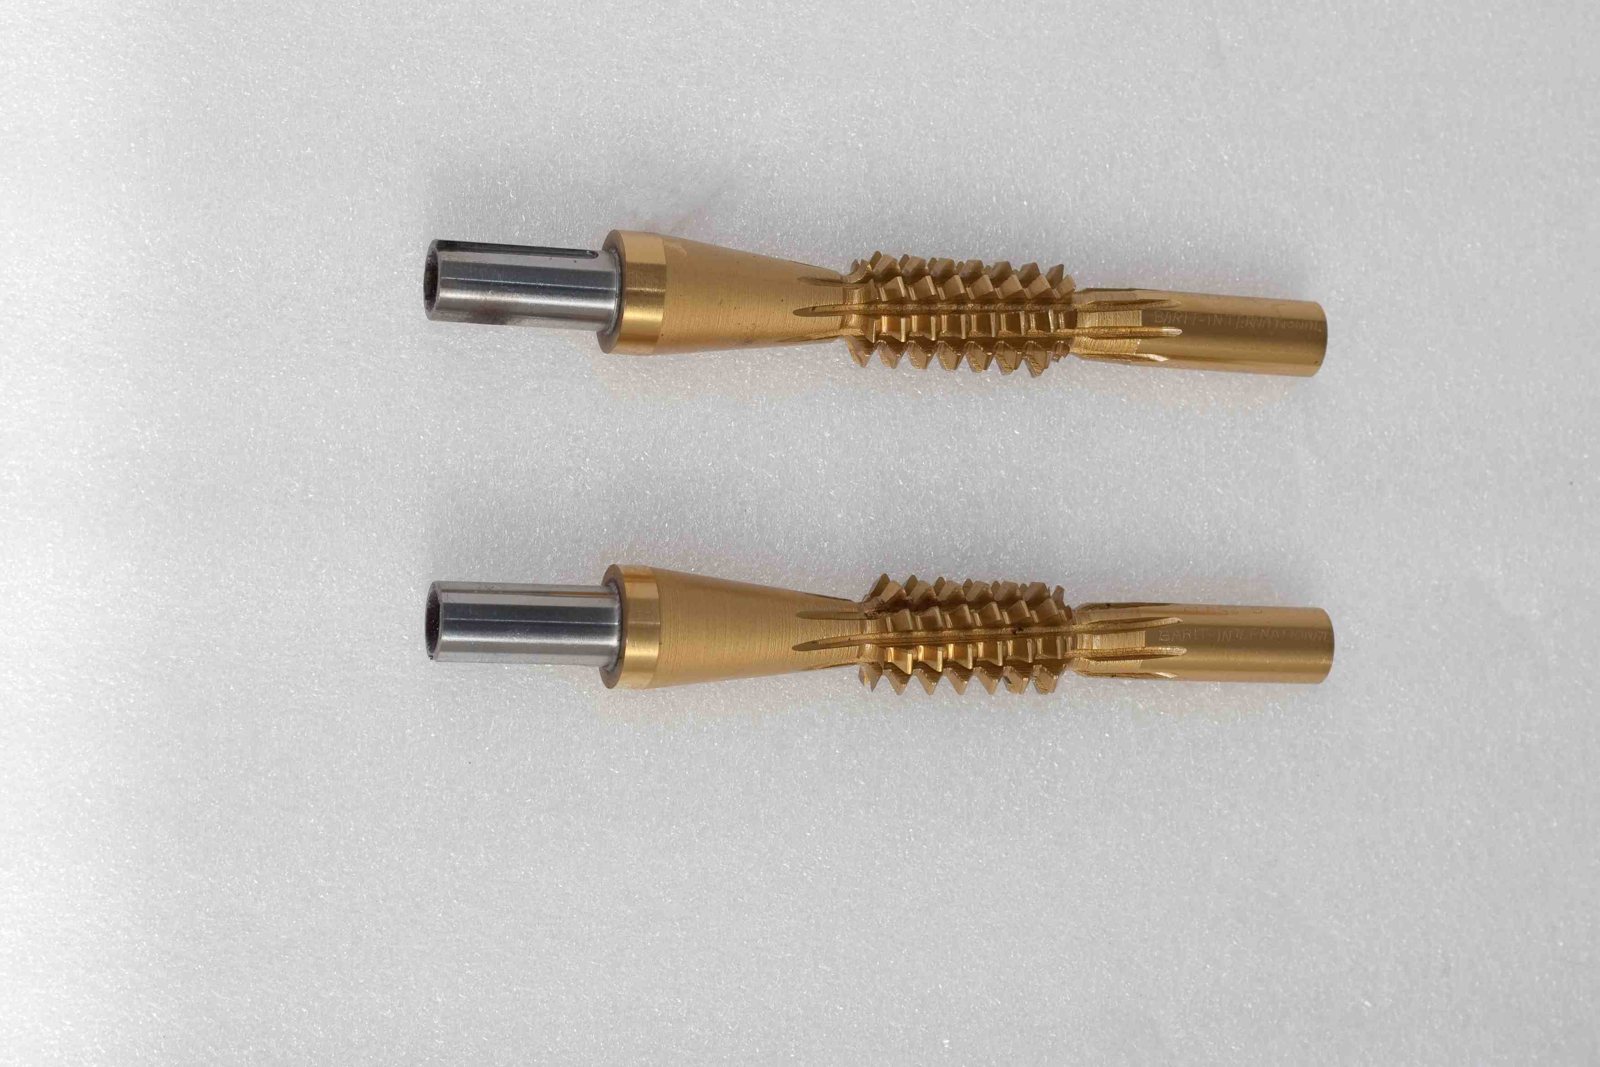
Hollow (bore-type) hobs
Mounted on the hobbing machine arbor like a gear hob. The usual choice for larger worm wheels and radial feed.
Shank-type hobs
An integral shank for stiffness and control, especially on small worm wheels and high lead angles where a bore-type hob would be too small to mount securely.
Tangential and radial feed hobs
Tangential-feed hobs carry a tapered lead-in and produce the most accurate worm-wheel tooth form; radial-feed hobs are faster for production work.
Topping and non-topping; reaming-type finishing hobs
Topping hobs cut the worm wheel outside diameter in the same pass. Reaming-type (finishing) hobs take a light final cut for the best surface finish and contact pattern.
Matching the hob to the worm
A worm gear hob must duplicate the worm it will mesh with: same axial module or pitch, pressure angle, number of starts, lead angle and flank form, with an oversize allowance for clearance. Send us the worm drawing and the worm wheel drawing and we will design the hob.
Applications
- Industrial gearboxes: speed reducers and winches.
- Automotive: steering and actuator drives.
- Robotics and automation: compact, self-locking drives.
Why buy CTI tooling through CTI-USA
- Matched to your worm. Flank form, lead angle, starts and oversize are taken from your worm and worm-wheel drawings so the contact pattern is right the first time.
- One manufacturer, every gear cutting tool. Hobs, shaper cutters, power skiving cutters, broaches and milling cutters from Capital Tool Industries, a single ISO 9001 source in Patiala, India, so profiles and tolerances are consistent across your process.
- Materials and coatings that fit the job. M2, M35, ASP 2030, ASP 2052, ASP 2060, S290 and S390 high-speed steels (conventional and powder-metallurgy); TiN, TiCN, TiAlN, AlCrN (Alcrona) and Altensa PVD coatings. Our engineers recommend the combination for your workpiece, hardness and volume. Properly specified coatings typically extend tool life 3–8× compared with uncoated tools.
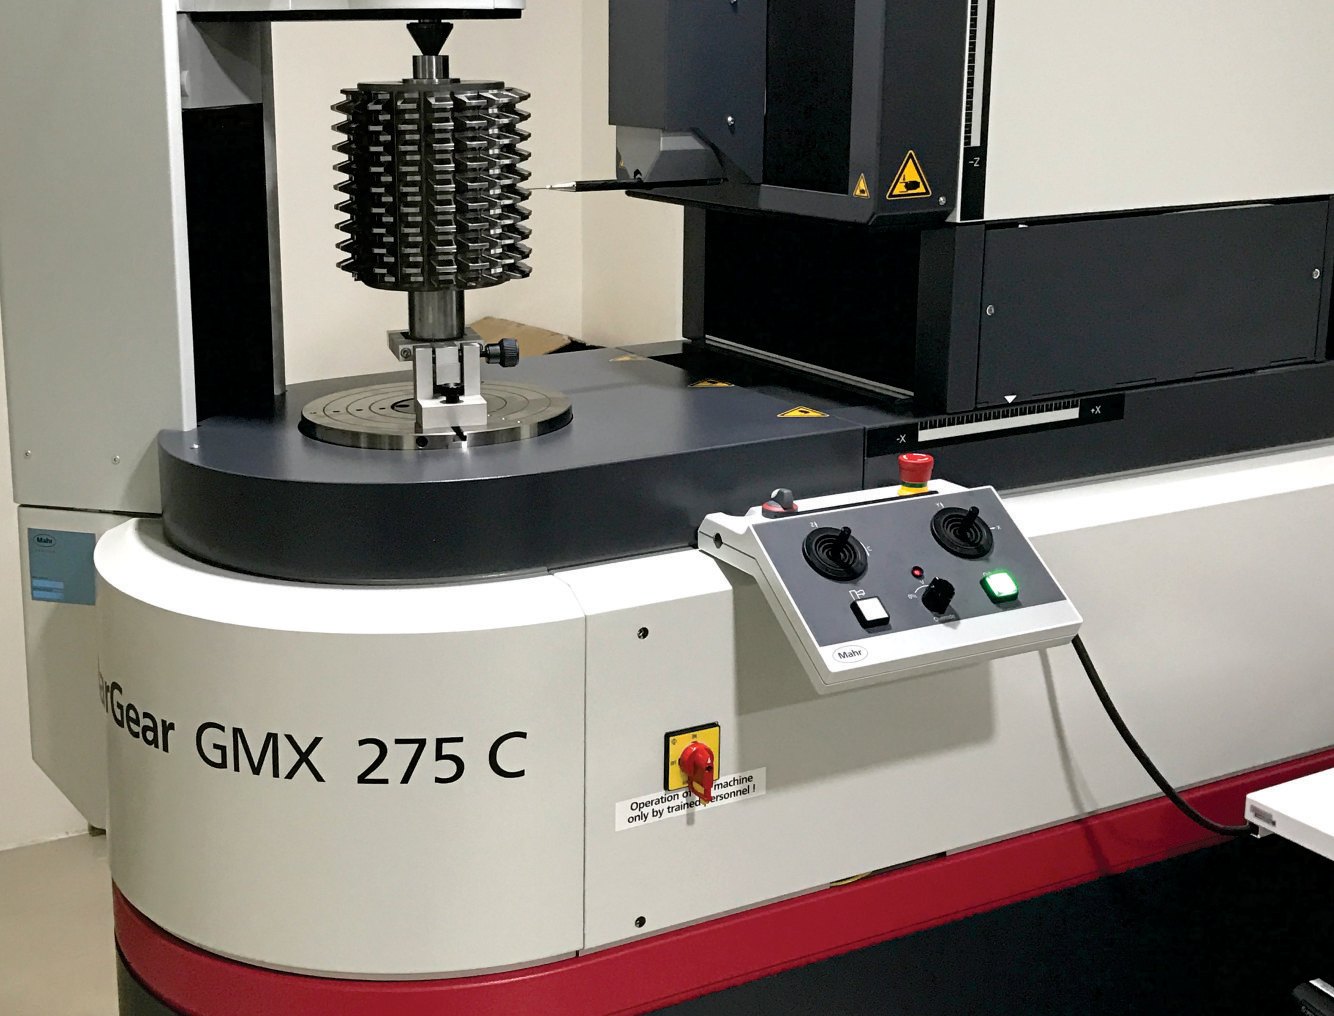
- Inspection you can read. Each tool is measured on Klingelnberg equipment and ships with its report.
- US-based support. Prints, technical questions and quotes are handled from Hudson, Ohio (Monday–Friday, 8:00 am–5:00 pm Eastern); we reply within one business day. Typical lead time is 6–8 weeks.
- Resharpening and recoating. We arrange resharpening and recoating of hobs, shaper cutters and broaches of any make, so you get the full regrind life out of every one.
Send us a print
Email a part drawing or tool drawing to sales@cti-usa.co or use the request-a-quote form (PDF, DWG, DXF, STEP, IGES or an image, up to 8 MB through the request form; larger files by email (ask for a transfer link over 20 MB)). Tell us the worm drawing (module or pitch, pressure angle, starts, lead angle, flank form), the worm wheel drawing, material, and volume, and we will recommend a tool steel and coating with the quote. We reply within one business day; typical lead time is 6–8 weeks.
Frequently asked questions
What flank forms do you make worm hobs for?
ZN, ZA, ZI (involute), ZK and ZC, up to a 45° lead angle.
Bore-type or shank-type?
Bore (hollow) hobs mount on the machine arbor and suit larger worm wheels. Shank hobs are stiffer and are used for small worm wheels and high lead angles.
What is a reaming-type worm hob?
A finishing hob that takes a light final cut after roughing, giving the best surface finish and contact pattern on the worm wheel.
What do you need to quote a worm gear hob?
The worm drawing (module or pitch, pressure angle, starts, lead angle, flank form) and the worm wheel drawing, plus the workpiece material and volume.
Related pages and guides
Send us a print and we will get started.
Our engineers will recommend the tool steel and coating for your job and quote it. Typical lead time 6–8 weeks.