Automated Gear Hobbing: The Eifco HOBBER 250 with Automatic Part Loading
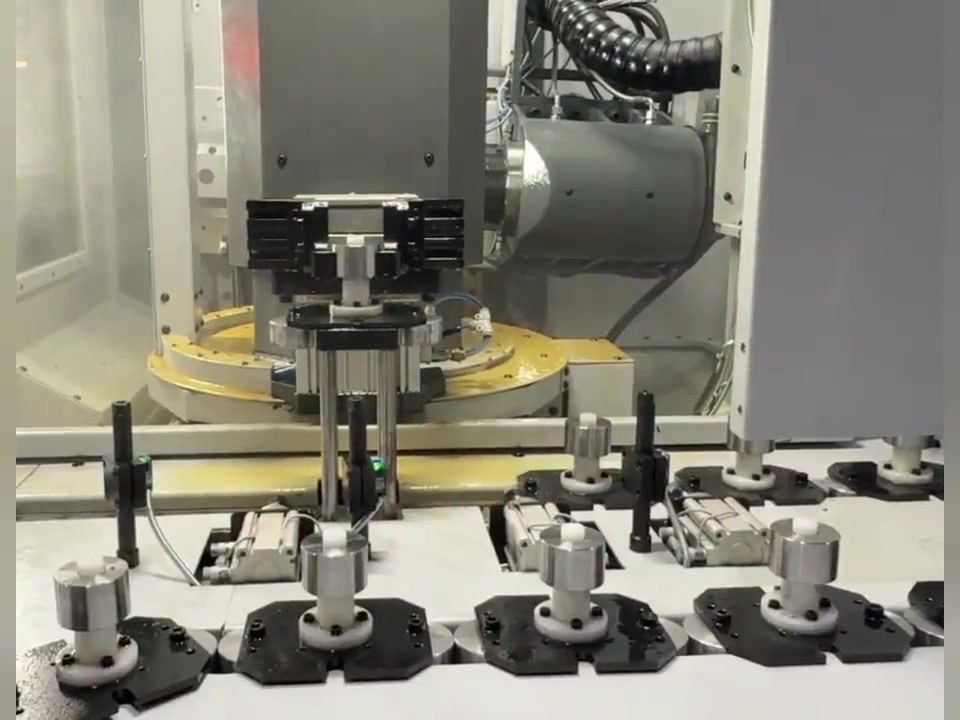
Eifco has just released footage of its HOBBER 250 CNC gear hobbing machine running with automatic part loading. It is worth thirty seconds of any gear shop's time, because it shows where gear hobbing is heading: machines that keep cutting while fewer, busier people look after them.
Why automation, and why now
Eifco's own point is one most gear shops will recognise: skilled operators are getting harder to find, and the experienced people who set up and tended hobbers for decades are not easily replaced. A machine that loads itself does not remove the need for skill. Someone still sets up the job, proves out the first part and checks the gears. What it removes is the hours spent standing at the machine swapping blanks, so one skilled person can keep several spindles cutting.
What the video shows
The cycle is simple. The hob cuts the gear under coolant. When the cycle ends, a gripper lifts the finished gear off the work table and sets it back on the fixture conveyor that runs past the machine. The conveyor indexes the next blank into position, the gripper places it on the table, and the machine starts the next cut. The operator's job becomes loading the conveyor, checking parts and changing hobs, not feeding the machine one blank at a time.
The machine
- Workpiece: up to 250 mm (9.8 in) diameter, on a 250 mm table
- Module: up to 6 in steel
- Drive: direct-drive hob and table spindles, hob speed up to 1,800 rpm, 29 kW (39 hp) hob spindle
- Travel and hob size: 500 mm vertical slide; hobs up to 150 mm diameter and 180 mm long; hob head swivel ±45°
- Control: Fanuc 0i-MF or Siemens Sinumerik CNC, specified at order, with 7 or 8 axes and an electronic gearbox in place of change gears
- Correction cycles: lead and span correction, crowning, taper and cluster cycles
- Weight: about 10 metric tons (22,000 lb)
The full specification, side by side with the rest of the HOBBER range from the 150 to the 630, is on our Eifco CNC gear hobbing machines page.
What it cuts
Spur and helical gears, splines, sprockets and worm wheels, up to module 6 in steel, loaded by hand or automatically. Eifco also highlights small pump gears with modified tooth profiles, a good example of the precision, high-volume work that suits an automated cell. The direct-drive spindles and available hob speeds also make dry hobbing practical, which removes coolant handling from the cell altogether.
When automatic loading pays
Automation earns its keep on repeat work. Before deciding, answer these for your parts:
- Batch size and changeovers. How many of the same part do you run at a time, and how often does the job change? Long runs of a few part families suit an autoloader best.
- Part family. Do your gears share a bore and a similar outside diameter, so one gripper and fixture set covers most of them?
- Cycle time. How long is the cut? Short cycles mean more loads per hour, which is where hand loading costs the most. Our free hobbing cycle-time estimator gives a quick first number.
- Upstream and downstream. How do blanks arrive from turning, and where do finished gears go for deburring and inspection?
- Inspection. How often must a part be checked, and by whom?
Send us the answers and your part prints, and we will review whether manual loading, automatic loading or a different HOBBER model fits.
Automation runs on tool life
An automated hobber cuts unattended for as long as the hob lasts, so tool life sets how long the cell can run between interventions. That makes the hob specification as important as the machine. CTI-USA supplies CTI hobs from module 0.1 to 40, in DIN 3968 class AA, A or B, with the tool steel and coating chosen for your material and volume, including powder-metallurgy steels and coatings such as TiAlN and Altensa for high-speed and dry cutting. A resharpening and recoating program keeps a set of hobs in rotation so the machine is never waiting for a tool.
Support in North America
CTI-USA is Eifco's North American distributor and service contact. We review the application, quote the machine and the tooling together, and coordinate installation and training at your plant by Eifco factory technicians. North American electrical requirements are confirmed at quotation, and delivery, warranty, service response and spare-parts arrangements are put in writing on every quote. For the full list of questions to settle before buying, read what to ask before you buy a CNC gear hobber.
See it for yourself
If you would like to talk through the HOBBER 250 or automated hobbing against your own parts, email sales@cti-usa.co, call 330-962-8160, or use the request form. Demonstrations can be arranged at Eifco in Coimbatore or at a North American installation.
Richard Potesta is the founder of CTI-USA, the North American sales, engineering and support partner of Capital Tool Industries and distributor for Eifco machines. Questions about an application? Contact CTI-USA or call 330-962-8160.
Considering automated hobbing?
Send us your part prints and volumes. We will review the HOBBER model, the loading and the hobs, and quote them together.